NM01X0AW0026
Choose Quantity
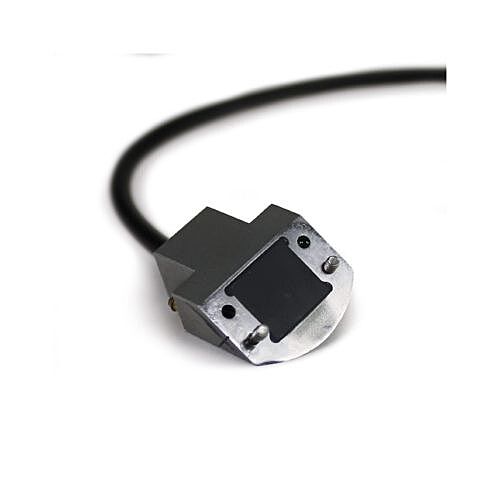
Sonatest — X0AW-N55S-IHC Ultrasonic Wedge
55° Shear-Wave Wedge, 39° Cut Angle, 0 mm Delay Line, 6 in AOD, for Compatible X0 Transducers
SKU: X0AW-002-6
Overview
The Sonatest X0AW-N55S-IHC is a 55-degree shear-wave ultrasonic wedge designed for angle-beam ultrasonic testing with compatible X0-series transducers.
Its acoustic geometry is specified for a nominal 55° refracted shear-wave angle in steel using a 39° physical cut angle. The wedge is also configured for a 6 in AOD (Axial Outside Diameter) application, making it suitable for inspections where the probe must conform to or be used on a cylindrical outside surface with approximately 6 in diameter.
With a 0 mm delay line, the wedge maintains the intended X0 acoustic configuration without an additional delay section. SKU X0AW-002-6 is intended for professional weld inspection, flaw detection, piping inspection, fabrication QA/QC, maintenance, and other industrial ultrasonic testing applications.
What's Included
| Item | Details |
|---|---|
| Ultrasonic Wedge | Sonatest X0AW-N55S-IHC |
| Wedge Series | X0 |
| Wave Type | S — Shear Wave |
| Nominal Refracted Angle in Steel | 55° |
| Physical Cut Angle | 39° |
| Delay Line | 0 mm |
| AOD | 6 in |
| Compatible Probe Type | Compatible X0-series transducers |
| Primary Application | Angle-beam ultrasonic inspection |
| Inspection Method | Ultrasonic Testing / UT |
| Manufacturer | Sonatest |
| SKU | X0AW-002-6 |
Note: Ultrasonic transducer, flaw detector, couplant, mounting hardware, calibration blocks, and other accessories are not included unless specified separately.
Box Dimensions & Shipping Weight (Estimated)
| Parameter | Imperial |
|---|---|
| Length | 6.0 in |
| Width | 4.0 in |
| Height | 3.0 in |
| Dimensions (L × W × H) | 6.0 × 4.0 × 3.0 in |
| Weight | 0.5 lb |
Actual shipping dimensions and weight may vary according to packaging and supplied hardware.
Key Specifications
| Parameter | Details |
|---|---|
| Product Type | Ultrasonic angle-beam wedge |
| Model | X0AW-N55S-IHC |
| Wedge Series | X0 |
| Wave Type | Shear Wave / S |
| Nominal Angle in Steel | 55° |
| Cut Angle | 39° |
| Delay Line | 0 mm |
| AOD | 6 in |
| Inspection Technique | Angle-beam ultrasonic testing |
| Compatible Transducer Family | X0-series compatible probes |
| Primary Use | Weld and flaw inspection |
| Coupling Method | Contact ultrasonic coupling |
| Inspection Method | Ultrasonic Testing / UT |
| Manufacturer | Sonatest |
| SKU | X0AW-002-6 |
Inspection Configuration
| Parameter | Details |
|---|---|
| Refracted Wave Mode | Shear wave |
| Nominal Refracted Angle in Steel | 55° |
| Physical Wedge Cut Angle | 39° |
| Delay-Line Length | 0 mm |
| AOD Configuration | 6 in cylindrical outside diameter |
| Typical Technique | Angle-beam pulse-echo inspection |
| Probe Mounting | Compatible X0 transducer mounted to wedge |
| Couplant Requirement | Appropriate ultrasonic couplant |
| Calibration Requirement | Wedge delay, sensitivity, index, and angle verification |
| Typical Inspection Target | Welds, fusion zones, cracks, and internal reflectors |
The stated 55° angle is referenced to steel. Actual refracted angle can vary when the wedge is used on materials with different acoustic velocities.
Performance Features
55° Shear-Wave Configuration
Provides a nominal 55-degree refracted shear-wave sound path in steel for conventional angle-beam ultrasonic inspection.
39° Physical Cut Angle
The wedge geometry is machined to a 39-degree cut angle to generate the intended 55° shear-wave path in steel.
6 in AOD Configuration
Designed for use on cylindrical outside surfaces with approximately 6 in outside diameter, supporting improved contact and coupling on curved components.
0 mm Delay Line
Specified without an additional delay-line section, preserving the intended X0 wedge geometry.
Designed for X0-Series Probes
Configured for use with compatible Sonatest X0 ultrasonic transducers.
Reusable Inspection Accessory
Can be used repeatedly when the contact surface, mounting surfaces, and acoustic interfaces remain in suitable condition.
Advantages of a 55° Shear-Wave Wedge
A 55-degree shear-wave configuration can provide useful sound paths for selected weld and structural applications.
Potential benefits include:
Directional examination of weld volumes
Evaluation of weld fusion zones
Detection of planar discontinuities
Inspection of reflectors not favorably oriented to straight-beam sound
Useful coverage between common 45° and 60° inspection angles
Support for multi-angle weld-inspection procedures
Practical sound paths for curved and cylindrical components
Compatibility with conventional pulse-echo flaw detection
The correct wedge angle should always be selected according to component thickness, weld geometry, material, inspection code, and written procedure.
AOD 6 in Configuration Advantages
The 6 in AOD specification is useful when inspecting cylindrical components with approximately 6 in outside diameter.
Potential benefits include:
Improved wedge contact on curved surfaces
More consistent coupling
Reduced rocking during scanning
Better probe stability
More repeatable sound entry
Practical use on piping and cylindrical components
Improved manual scanning control
Better fit compared with a flat-bottom wedge on a curved surface
Actual fit depends on the true outside diameter, surface condition, and wedge contour.
User-Friendly Design
Fixed 55° shear-wave configuration
Defined 39° cut angle
0 mm delay-line specification
6 in AOD contour
Designed for compatible X0 transducers
Suitable for field and shop inspection
Supports repeatable angle-beam setups
Suitable for manual weld scanning
Supports conventional calibration procedures
Fixed 55° shear-wave configuration
Defined 39° cut angle
0 mm delay-line specification
6 in AOD contour
Designed for compatible X0 transducers
Suitable for field and shop inspection
Supports repeatable angle-beam setups
Suitable for manual weld scanning
Supports conventional calibration procedures
Built for Industrial Inspection
Designed for professional ultrasonic testing
Suitable for piping and weld inspection
Practical for fabrication and maintenance applications
Supports structural and QA/QC inspection workflows
Useful for curved and cylindrical components
Suitable for repeated manual scanning
Can be incorporated into documented inspection procedures
Intended for use with proper calibration and ultrasonic couplant
Designed for professional ultrasonic testing
Suitable for piping and weld inspection
Practical for fabrication and maintenance applications
Supports structural and QA/QC inspection workflows
Useful for curved and cylindrical components
Suitable for repeated manual scanning
Can be incorporated into documented inspection procedures
Intended for use with proper calibration and ultrasonic couplant
Compatibility
Compatible with:
Appropriate Sonatest X0-series transducers
Compatible ultrasonic flaw detectors
Conventional pulse-echo angle-beam systems
Suitable ultrasonic couplants
IIW and other applicable calibration blocks
Weld-inspection procedures
Carbon steel and other suitable materials
Cylindrical components near 6 in outside diameter
Field and laboratory ultrasonic-testing programs
Transducer fit, mounting hardware, frequency, material, required refracted angle, actual component diameter, and instrument compatibility should be confirmed before ordering.
Ideal Applications
Pipeline weld inspection
Pipe weld inspection
Circumferential weld inspection
Structural weld evaluation
Fabrication QA/QC
Pressure-vessel inspection
Cylindrical component inspection
Storage-tank weld inspection
Structural steel inspection
Machinery-component evaluation
Maintenance inspection
Crack detection
Lack-of-fusion evaluation
Angle-beam flaw detection
Field ultrasonic testing
Pipeline weld inspection
Pipe weld inspection
Circumferential weld inspection
Structural weld evaluation
Fabrication QA/QC
Pressure-vessel inspection
Cylindrical component inspection
Storage-tank weld inspection
Structural steel inspection
Machinery-component evaluation
Maintenance inspection
Crack detection
Lack-of-fusion evaluation
Angle-beam flaw detection
Field ultrasonic testing
Typical Discontinuities Evaluated
When used with a properly calibrated ultrasonic system, the X0AW-N55S-IHC can support evaluation of discontinuities such as:
Cracks
Lack of fusion
Incomplete penetration
Slag inclusions
Planar reflectors
Weld-related discontinuities
Service-induced cracking
Other internal reflectors favorably oriented to the 55° sound beam
Detectability depends on flaw size, orientation, depth, material properties, transducer frequency, sound path, and inspection technique.
Inspection Guidelines
Verify compatibility between the wedge and X0 transducer
Confirm that the 6 in AOD contour matches the component geometry
Inspect the contact surface before use
Mount the transducer securely
Apply coupling material between interfaces when required
Apply suitable ultrasonic couplant to the test surface
Calibrate wedge delay, range, and sensitivity
Verify the probe index or exit point when required
Confirm the refracted angle using an appropriate reference block
Scan the required inspection area systematically
Maintain consistent wedge orientation on the curved surface
Record relevant indications and sound-path information
Recheck calibration periodically during inspection
Verify compatibility between the wedge and X0 transducer
Confirm that the 6 in AOD contour matches the component geometry
Inspect the contact surface before use
Mount the transducer securely
Apply coupling material between interfaces when required
Apply suitable ultrasonic couplant to the test surface
Calibrate wedge delay, range, and sensitivity
Verify the probe index or exit point when required
Confirm the refracted angle using an appropriate reference block
Scan the required inspection area systematically
Maintain consistent wedge orientation on the curved surface
Record relevant indications and sound-path information
Recheck calibration periodically during inspection
Angle and Material Considerations
The nominal 55° shear-wave angle is specified for steel.
When used on another material:
The refracted angle may change
Material sound velocity must be considered
Calibration should be performed on an appropriate reference standard
Actual beam behavior should be verified before inspection
Sound-path calculations should use the test material properties
Acceptance criteria should follow the governing inspection procedure
The physical 39° wedge cut angle should not be interpreted as the ultrasonic refracted angle inside the component.
Wedge Wear and Calibration
Wedge wear can affect sound entry point, refracted angle, curvature fit, wedge delay, and inspection accuracy.
For reliable performance:
Inspect the contact surface regularly
Keep the wedge face clean
Avoid excessive abrasion
Verify wedge delay periodically
Confirm the exit point when required
Recheck the refracted angle as appropriate
Monitor the 6 in AOD contour for uneven wear
Recalibrate after replacing the wedge
Replace heavily worn or damaged wedges
Avoid unauthorized grinding or reshaping
Care and Handling
Avoid dropping or striking the wedge
Keep coupling surfaces clean
Remove couplant after inspection
Inspect mounting surfaces for damage
Protect the curved contact face from scratches
Do not modify the 39° cut geometry or 6 in AOD contour
Store in a clean, dry location
Keep protected during transportation
Verify transducer fit before inspection
Replace the wedge if wear affects calibration or sound transmission
Avoid dropping or striking the wedge
Keep coupling surfaces clean
Remove couplant after inspection
Inspect mounting surfaces for damage
Protect the curved contact face from scratches
Do not modify the 39° cut geometry or 6 in AOD contour
Store in a clean, dry location
Keep protected during transportation
Verify transducer fit before inspection
Replace the wedge if wear affects calibration or sound transmission
About Sonatest
Sonatest develops ultrasonic flaw detectors, phased-array systems, transducers, wedges, scanners, and related accessories for professional non-destructive testing. Its products support weld inspection, pipeline inspection, fabrication, manufacturing, maintenance, structural evaluation, asset integrity, and industrial quality-control applications.